7 Best Sustainable Dyeing Processes for Global Buyers

Choosing a dyeing method is no longer only a question of color, cost, or production speed. Global buyers increasingly examine water use, chemical management, worker safety, energy demand, and traceability before approving a supplier. A credible sustainable dyeing process must perform in the factory, not merely appear attractive in marketing materials.

This guide examines seven dyeing processes used across apparel, home textiles, and technical fabrics. It considers practical details, including wastewater treatment, salt reduction, low-temperature operation, recycled water, and compatibility with natural or synthetic fibers. Some methods can reduce resource consumption, while others may require specialized machinery, longer sampling periods, or stricter process control. Results also depend on fiber quality, dye selection, equipment condition, and local infrastructure.

There is no perfect solution.

Experienced sourcing teams know that laboratory claims can change on a busy production line. Shade variation may appear between dye lots. Supplier records may also be incomplete, especially across complex supply chains. These limitations deserve honest attention, not polished promises. Buyers should request test reports, chemical inventories, wastewater data, and recognized certifications where appropriate. They should also inspect corrective actions rather than accepting documents without verification.

The following overview offers a practical starting point for responsible procurement. It connects technical performance with commercial reality, helping buyers compare options more carefully. The best choice may not be the newest process. It may be the one a supplier can operate consistently, document clearly, and improve over time.

7 Best Sustainable Dyeing Processes for Global Buyers

What Makes a Dyeing Process Sustainable for Global Buyers

7 Best Sustainable Dyeing Processes for Global Buyers

What Makes a Dyeing Process Sustainable for Global Buyers

Sustainability starts with measurable impact, not attractive claims. Textile Exchange reported 124 million tonnes of global fiber production in 2023. That scale makes dyeing efficiency commercially important. UNEP estimates textiles create 2–8% of global greenhouse gas emissions. Water, heat, chemicals, and wastewater all matter.

Seven processes deserve careful screening: low-liquor dyeing, air-flow dyeing, foam application, digital pigment printing, dope dyeing, supercritical carbon dioxide dyeing, and enzyme-assisted dyeing. Dope dyeing can reduce water use because color enters the polymer before extrusion. Digital pigment systems may reduce bath water and washing steps. Supercritical carbon dioxide can avoid conventional water baths, but its equipment demands high investment and skilled maintenance.

The best option depends on fiber, shade, order size, and factory infrastructure. A low-water process is not automatically sustainable. It may transfer pressure toward electricity, chemical purity, or difficult quality control. ZDHC’s wastewater guidance emphasizes chemical management, testing, and transparent discharge control. Buyers should request water and energy data per kilogram, restricted-substance test results, wastewater records, and batch-level traceability. Results should be independently verified when possible.

Perfect dyeing does not exist. Some factories still rely on estimates instead of meters. That weakness deserves honest reporting. Cost, colorfastness, and production speed must be tested together, preferably through pilot orders before global adoption.

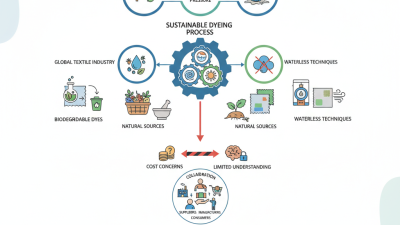
Seven Sustainable Dyeing Methods and Their Working Principles

Seven sustainable dyeing methods are changing how global buyers assess textile suppliers.

Their principles differ, but each targets water, energy, chemicals, or waste.

Low-liquor dyeing uses less bath water through tighter machine ratios.

Cold pad-batch dyeing applies reactive dye at room temperature, then fixes it slowly.

Dope dyeing adds pigment before synthetic fibre extrusion, reducing repeated wet treatments.

Digital pigment printing places colour only where required, limiting wastewater and fabric loss.

Supercritical carbon dioxide uses pressurised CO₂ instead of water for selected synthetic fibres. The CO₂ circulates in a closed loop.

Enzymatic dyeing uses biological catalysts to prepare or colour fibres under milder conditions.

Natural dyeing uses plant or mineral sources, although shade consistency and crop impacts require careful testing.

UNEP’s 2023 Sustainability and Circularity in Textiles report estimates textiles create 2–8% of global greenhouse-gas emissions. The European Environment Agency also identifies wet processing as a major source of water, energy, and chemical pressure.

These figures make process selection commercially important, not merely fashionable. Yet no method is automatically sustainable. Dope dyeing may suit polyester, but not cotton. Natural dyes can require land, water, and mordants. The uncomfortable part is often ignored.

Tips: Ask suppliers for liquor ratios, energy use per kilogram, wastewater results, and colourfastness data. Request recent laboratory or third-party evidence. Compare the same fibre, shade, and production volume. A beautiful sample can hide a poor process. Keep questioning it.

How Water, Energy, Chemicals, and Waste Shape Sustainability

7 Best Sustainable Dyeing Processes for Global Buyers

How Water, Energy, Chemicals, and Waste Shape Sustainability

Sustainable dyeing is not one perfect solution. Buyers should compare seven options: low-liquor dyeing, cold pad-batch, foam dyeing, digital pigment printing, dope dyeing, supercritical carbon dioxide dyeing, and carefully managed natural dyes. Each process changes the factory’s water, energy, chemical, and waste profile.

Low-liquor machines can reduce water use significantly. Cold pad-batch dyeing also lowers heat demand for suitable cotton fabrics. Foam dyeing uses less water, but stable foam control requires technical skill. Digital pigment printing can reduce wastewater from traditional baths. Dope dyeing avoids a later wet process, yet it only works with selected synthetic fibers. Supercritical carbon dioxide dyeing uses almost no process water, although equipment costs remain high. Natural dyes may sound safer, but mordants and inconsistent shades need strict control.

Numbers matter more than attractive claims. Ask for water consumption per kilogram of fabric. Request energy data, chemical inventories, and wastewater test results. Check whether salt, alkali, and dye residues are recovered or discharged. Small details reveal performance: a stained drain, mixed chemical drums, or wet fabric waiting under a hot dryer.

Some factories measure production accurately. Others estimate. That weakness deserves attention. A buyer can require monthly records, independent testing, and corrective plans. Certification helps, but it cannot replace a site visit. The most sustainable process may still create waste when operators over-dye faulty fabric. Mistakes happen. Transparent reporting makes improvement possible.

Quality, Certification, and Compliance Standards for Global Sourcing

7 Best Sustainable Dyeing Processes for Global Buyers

Quality, Certification, and Compliance Standards for Global Sourcing

For global buyers, sustainable dyeing must protect quality and compliance together. Textile Exchange’s Materials Market Report 2024 recorded 124 million tonnes of global fiber production in 2023. It projects nearly 160 million tonnes by 2030. This scale makes chemical control, wastewater evidence, and shade consistency essential. Low-liquor dyeing, solution dyeing, digital printing, and certified natural dyes can reduce resource use. They are not automatically safer. A lower water bill cannot excuse poor fixation or restricted substances.

Require documented recipes, batch records, fiber details, and test results for every production lot. Check colorfastness, shrinkage, pH, formaldehyde, heavy metals, and aryl amines through ISO-aligned laboratories. The ZDHC Manufacturing Restricted Substances List supports chemical screening before bulk production. For organic claims, Global Organic Textile Standard certification should cover processing, not only fiber content. Ask for certificate scope, expiry dates, transaction records, and corrective-action closure. Paperwork is not enough. Walk through the dye house.

Wastewater reports should include COD, BOD, color, salts, temperature, flow, sampling dates, and laboratory identity. ISO 14001 supports environmental management, but it does not certify a specific dye recipe. The 2023 Fashion Transparency Index assessed 250 companies and reported an average transparency score of 26 percent. That gap matters. Audits can miss night shifts, subcontracting, or diluted samples. Approve pilot lots, set shade tolerances, and arrange independent retesting. Record every exception, responsible owner, deadline, and retest date.

7 Best Sustainable Dyeing Processes for Global Buyers - Quality, Certification, and Compliance Standards for Global Sourcing

Comparative sourcing guide for evaluating dyeing technologies, product quality, certification evidence, and international compliance requirements.

Rank / Dyeing Process How It Reduces Environmental Impact Best-Suited Fibers or Products Typical Resource Profile Quality and Performance Considerations Relevant Certification or Verification Key Compliance Requirements Buyer Due-Diligence Checks
1. Dope Dyeing
Solution or pigment coloration before synthetic-fiber extrusion
Color is incorporated into the polymer before filament formation, which can eliminate or greatly reduce a separate aqueous dye bath and associated wastewater. Polyester, polyamide, polypropylene, acrylic, and other melt-spun synthetic fibers; suitable for yarns, fabrics, and technical textiles. Very low process-water demand compared with conventional exhaust dyeing. Energy is still required for polymer melting and extrusion; pigment or masterbatch selection affects resource performance. Usually good shade consistency and colorfastness. Late-stage shade changes are difficult, and minimum production quantities may be higher. Recycled polymer feedstock can require tighter color and contamination control. Fiber or product certification under GRS or RCS where recycled content is claimed; OEKO-TEX Standard 100 for harmful-substance testing; ISO 14001 may verify environmental-management systems. Chemical restrictions under REACH where applicable, restricted-substance requirements in the destination market, accurate recycled-content claims, and traceability of polymer inputs. Request fiber-production records, color masterbatch specifications, recycled-content transaction evidence, colorfastness reports, and wastewater records for any downstream wet processing.
2. Digital Pigment Printing
Inkjet application of pigment inks with controlled curing
Applies color only where required, reducing screen preparation, wash-off, print-paste waste, and water used for cleaning compared with many conventional printing routes. Cotton, polyester, blends, and selected cellulosic or synthetic fabrics, subject to ink and pretreatment compatibility. Generally low water use during printing; energy demand depends on pretreatment and curing. Unused ink, cartridges, coatings, and cleaning fluids require controlled disposal. Supports short runs, detailed graphics, and rapid sampling. Durability depends on pigment adhesion, binder formulation, curing temperature, rubbing, washing, and fabric preparation. OEKO-TEX Standard 100 for finished-product harmful-substance testing; GOTS or bluesign system requirements may apply when the full product and process meet their criteria; ISO 9001 can support process control. Chemical restrictions, labeling rules, wastewater and air-emission controls, and truthful claims regarding organic fibers, recycled content, or preferred chemicals. Check ink safety data sheets, curing records, wash and rub fastness, print-reproduction tolerances, pretreatment controls, and disposal documentation for consumables.
3. Air Dyeing
Air-assisted coloration of selected synthetic textiles
Uses air as the primary transfer medium rather than a conventional water bath, potentially reducing water consumption and dye liquor discharge. Primarily polyester and other suitable synthetic fabrics engineered for air-dyeing equipment; suitability varies by construction and dye class. Low water requirement during coloration, but electricity and thermal energy can be material. Overall impact depends on machine efficiency, drying, and heat-setting conditions. Can provide even shades when fabric permeability and airflow are controlled. Evaluate shade penetration, barré, migration, crease marks, and batch-to-batch reproducibility. OEKO-TEX Standard 100 for finished goods; ISO 14001 for environmental management; facility-level water and chemical data should be independently verified because no universal “air-dyed” certification exists. Destination-market chemical restrictions, wastewater requirements for pretreatment or finishing stages, energy and emissions reporting, and substantiation of water-saving claims. Obtain water and energy consumption per kilogram, machine specifications, shade reproducibility data, fastness reports, and a calculation method for environmental claims.
4. Supercritical CO₂ Dyeing
Pressurized carbon dioxide as a dye-transfer medium
Can operate without a conventional water dye bath, with CO₂ recovered and reused in a closed-loop system when the equipment is properly operated. Primarily hydrophobic synthetic fibers such as polyester; performance depends on dye compatibility and fabric construction. Very low direct water use and minimal aqueous effluent during dyeing. High-pressure equipment and heating require significant capital and energy management. Can achieve strong color penetration and reproducibility on suitable substrates. Shade matching, equipment capacity, pressure control, and limited fiber applicability require specialist expertise. OEKO-TEX Standard 100 for finished-product safety; ISO 14001 or ISO 50001 may support environmental and energy management; process claims should be supported by site-level measurements. Pressure-equipment safety, chemical restrictions, worker protection, energy and greenhouse-gas accounting, and accurate disclosure of whether CO₂ is recovered or externally sourced. Verify closed-loop recovery rates, energy intensity, dye fixation, colorfastness, equipment safety inspections, and lifecycle boundaries used in environmental comparisons.
5. Low-Liquor-Ratio Dyeing
Optimized aqueous dyeing with reduced bath ratio
Reduces the quantity of water, salt, auxiliaries, heating, and wastewater generated per kilogram by using a smaller dye liquor volume and improved dosing control. Cotton, viscose, wool, nylon, polyester, and blends, provided the machine and dye class are correctly matched. Water and chemical savings vary by machine, substrate, shade depth, and recipe. Requires effective bath control, heat recovery, and wastewater treatment to maximize benefits. Established technology with broad shade availability. Risks include unevenness, crease marks, poor leveling, or reduced reproducibility if loading and liquor circulation are not controlled. GOTS, bluesign system, or OEKO-TEX-related requirements may be relevant depending on the complete product and chemical inputs; ISO 14001 supports environmental-management verification. Chemical inventory control, wastewater discharge limits, restricted-substance management, worker safety, and documentation of organic or recycled-fiber claims where applicable. Request liquor-ratio records, recipe sheets, water and chemical intensity per kilogram, laboratory fastness tests, wastewater test results, and corrective-action records.
6. Enzyme-Assisted Dyeing and Finishing
Biocatalysts used to improve preparation or coloration efficiency
Enzymes can enable lower-temperature preparation, reduce harsh chemical use, improve absorbency, or shorten selected wet-processing steps. Especially relevant to cotton and other cellulosic fibers; specific enzymes are also used in selected wool, linen, denim, and blended-textile processes. Potential reductions in temperature, processing time, and selected chemicals. Water savings depend on whether rinsing and subsequent dyeing steps are also optimized. Can improve absorbency, handle, or surface appearance. Excess treatment may reduce strength, alter weight, create unevenness, or affect dimensional stability. GOTS-approved chemical inputs may be relevant for certified organic textile products; OEKO-TEX Standard 100 tests the finished article; ISO 14001 supports facility controls. Chemical safety data, biological-agent handling, wastewater controls, product safety testing, and accurate claims that distinguish enzyme use from broader sustainability performance. Review enzyme technical data sheets, dosage and deactivation controls, temperature and pH logs, fabric-strength testing, absorbency results, and wastewater monitoring.
7. Natural and Bio-Based Dyeing
Colorants derived from plant, mineral, microbial, or other biological sources
Can reduce dependence on fossil-derived colorants when feedstocks are responsibly sourced and processed; some systems use agricultural by-products or renewable raw materials. Cotton, linen, hemp, wool, silk, and selected regenerated fibers; performance depends on the colorant, mordant, substrate, and application method. Resource use varies widely. Extraction may require substantial water, heat, or solvents, and some mordants can create hazardous residues. Renewable origin does not automatically mean low impact. Often provides distinctive, naturally variable shades. Light, wash, perspiration, and rubbing fastness may be lower or more variable than conventional dyes unless carefully engineered and tested. GOTS may apply to certified organic textile products and approved chemical inputs; OEKO-TEX Standard 100 can verify finished-product safety; organic-content certifications require documented chain of custody. Substantiate bio-based or natural-origin claims, control mordants and auxiliaries, comply with chemical restrictions, and document agricultural sourcing, biodiversity, land-use, and wastewater risks where relevant. Ask for botanical or feedstock origin records, extraction process data, mordant specifications, restricted-substance tests, full fastness testing, shade-tolerance standards, and chain-of-custody evidence.

Global buyer note: Certifications generally verify the product, facility, chemical inputs, management system, or chain of custody—not the dyeing process alone. Confirm the certification scope, certificate validity, transaction records, laboratory reports, and destination-market requirements before making sustainability or compliance claims.

How to Select the Best Dyeing Process for Each Textile Application

Selecting a sustainable dyeing process starts with the textile, not marketing language. In production trials, fiber content, fabric weight, shade depth, and order size changed the best option. Cotton jersey often suits fiber-reactive dyeing with optimized salt and alkali recovery. It delivers strong wash fastness, but wastewater treatment remains essential. For polyester sportswear, dope or solution dyeing can reduce water use when colors are forecast accurately. That condition matters. Overstock can erase environmental gains.

For delicate wool, low-temperature acid dyeing may protect handle and reduce rework. Small batches may benefit from digital pigment printing, especially for detailed patterns and sampling. Yet pigment systems can feel stiffer and need careful binder selection. Hemp and linen require controlled pretreatment because uneven absorbency can create barre effects. Natural dyes may fit premium, low-volume products, but shade consistency and light fastness need documented testing. They are not automatically sustainable.

Buyers should request process data per kilogram: water, energy, chemicals, wastewater load, and defect rate. Ask for laboratory reports, bulk trial results, and test methods, not broad claims. Check colorfastness after washing, rubbing, perspiration, and light exposure. A process that looks efficient in the lab may behave differently on a 500-kilogram lot. I have made that mistake. Leave room for corrective dyeing, because real fabric rarely follows the first recipe perfectly. Compare transport, drying temperature, and expected product life before approving the process.

7 Best Sustainable Dyeing Processes for Global Buyers

Typical freshwater use by textile dyeing process

The chart uses representative midpoints from published textile-processing ranges. Lower freshwater use generally indicates lower water demand, but final selection should also consider fiber type, color depth, fastness, wastewater treatment, production scale, and required hand feel.

Typical ranges referenced from textile environmental studies and industry guidance, including the European Commission Textile BREF and water-efficiency assessments. Actual consumption varies by machinery, recipe, fabric construction, and operating conditions.

Scroll to Top